
FMCG Packaging
High-volume packaging that balances shelf appeal, speed and cost per unit.
Customer Challenges
At volume, every gram and every second counts.
FMCG packaging has to win on cost, speed, shelf and sustainability at once.
Cost-per-unit pressure
High volumes magnify every cent of packaging cost.
Shelf stand-out
Products must catch the eye on a crowded shelf.
Line speed & automation
Packaging must run on existing high-speed lines.
Recyclability demands
Retailers and regulators require recyclable materials.
Supply continuity
Stock-outs are costly; supply must stay secure at scale.
Throughput consistency
Quality must hold at high run rates.
Konix Solution
Shelf appeal and cost per unit — engineered for scale.
We engineer brand-forward retail packaging plus cost-optimised protective trays that balance material cost, line speed and recyclability — produced across multiple sites to keep your supply secure at volume.
- Brand-forward, high-clarity retail packaging.
- Material- and weight-optimised for cost per unit.
- Designed to run at your line speed and automation.
- Recyclable / bio-based options and multi-site supply.
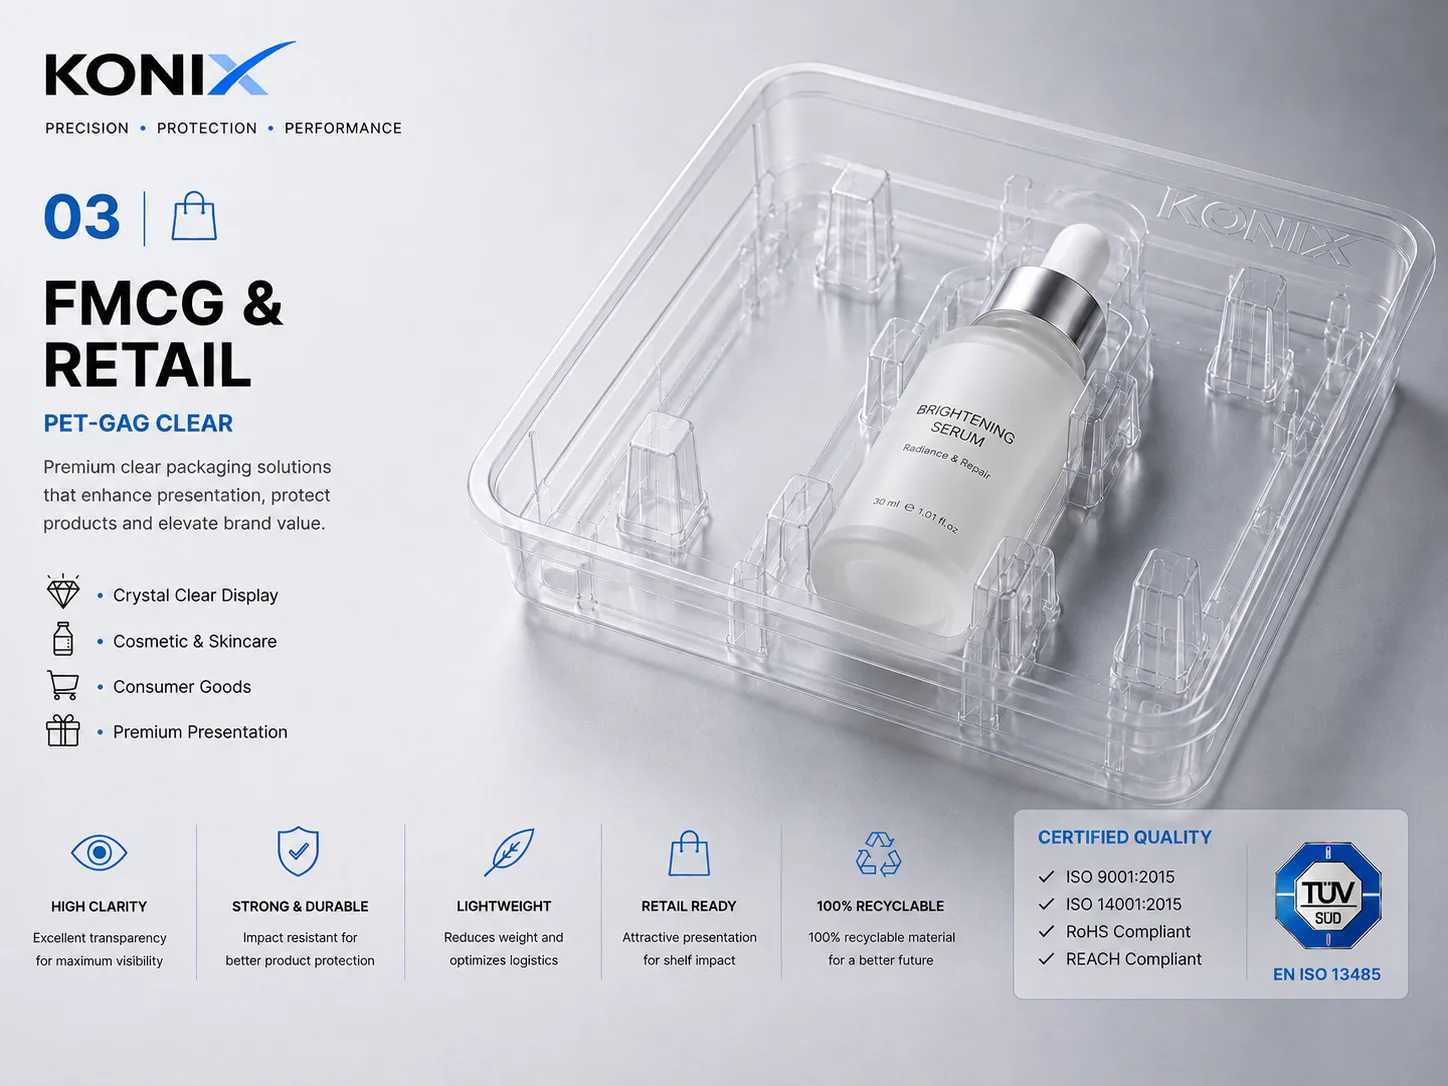
Applications
Formats we engineer for FMCG.
Business Benefits
What it means for your KPIs.
Lower cost per unit
Material and weight optimisation at volume protects margin.
PurchasingShelf stand-out
Brand-forward packaging that lifts shelf presence.
MarketingThroughput held
Packs engineered to run at line speed keep output steady.
ManufacturingRecyclability targets
Recyclable / bio-based options meet retailer and regulator demands.
Sustainability / HQEngineering Features
The engineering behind the pack.
Light-weighting
Material reduction without losing protection or appeal.
Line-speed design
Packs engineered to your filling-line and automation.
Recyclable / bio-based
Materials qualified for recyclability targets (TEXa Bio).
High-clarity retail
Brand-forward, display-ready presentation.
Multi-site supply
Regional capacity to secure supply at volume.
Validation & QA
Throughput and protection validated at run rate.
Case Study
Brand — more sustainable, same shelf appeal, same line.
A brand needed a more sustainable pack that kept shelf appeal, ran on existing lines and held cost per unit.
A light-weighted, recyclable pack validated for the line and produced across multiple sites.
Recyclability targets met · throughput held · cost per unit kept in line.
Outcomes are directional and vary by product, line and material scope. We model the expected trade-off with you before tooling.
FAQ
FMCG packaging questions.
Can you cut cost per unit without losing shelf appeal?
Will packs run on our existing lines?
Do you offer recyclable or bio-based materials?
Can you secure supply at volume?
Request a Solution
Scaling a product and watching cost per unit? Let's optimise your packaging.
Our engineers will optimise for cost, shelf and sustainability — a recommendation, not a generic quote. A local engineering team in Đồng Nai. Your drawings and data stay confidential.